Pump Trolleys with Retractable Hose Reels
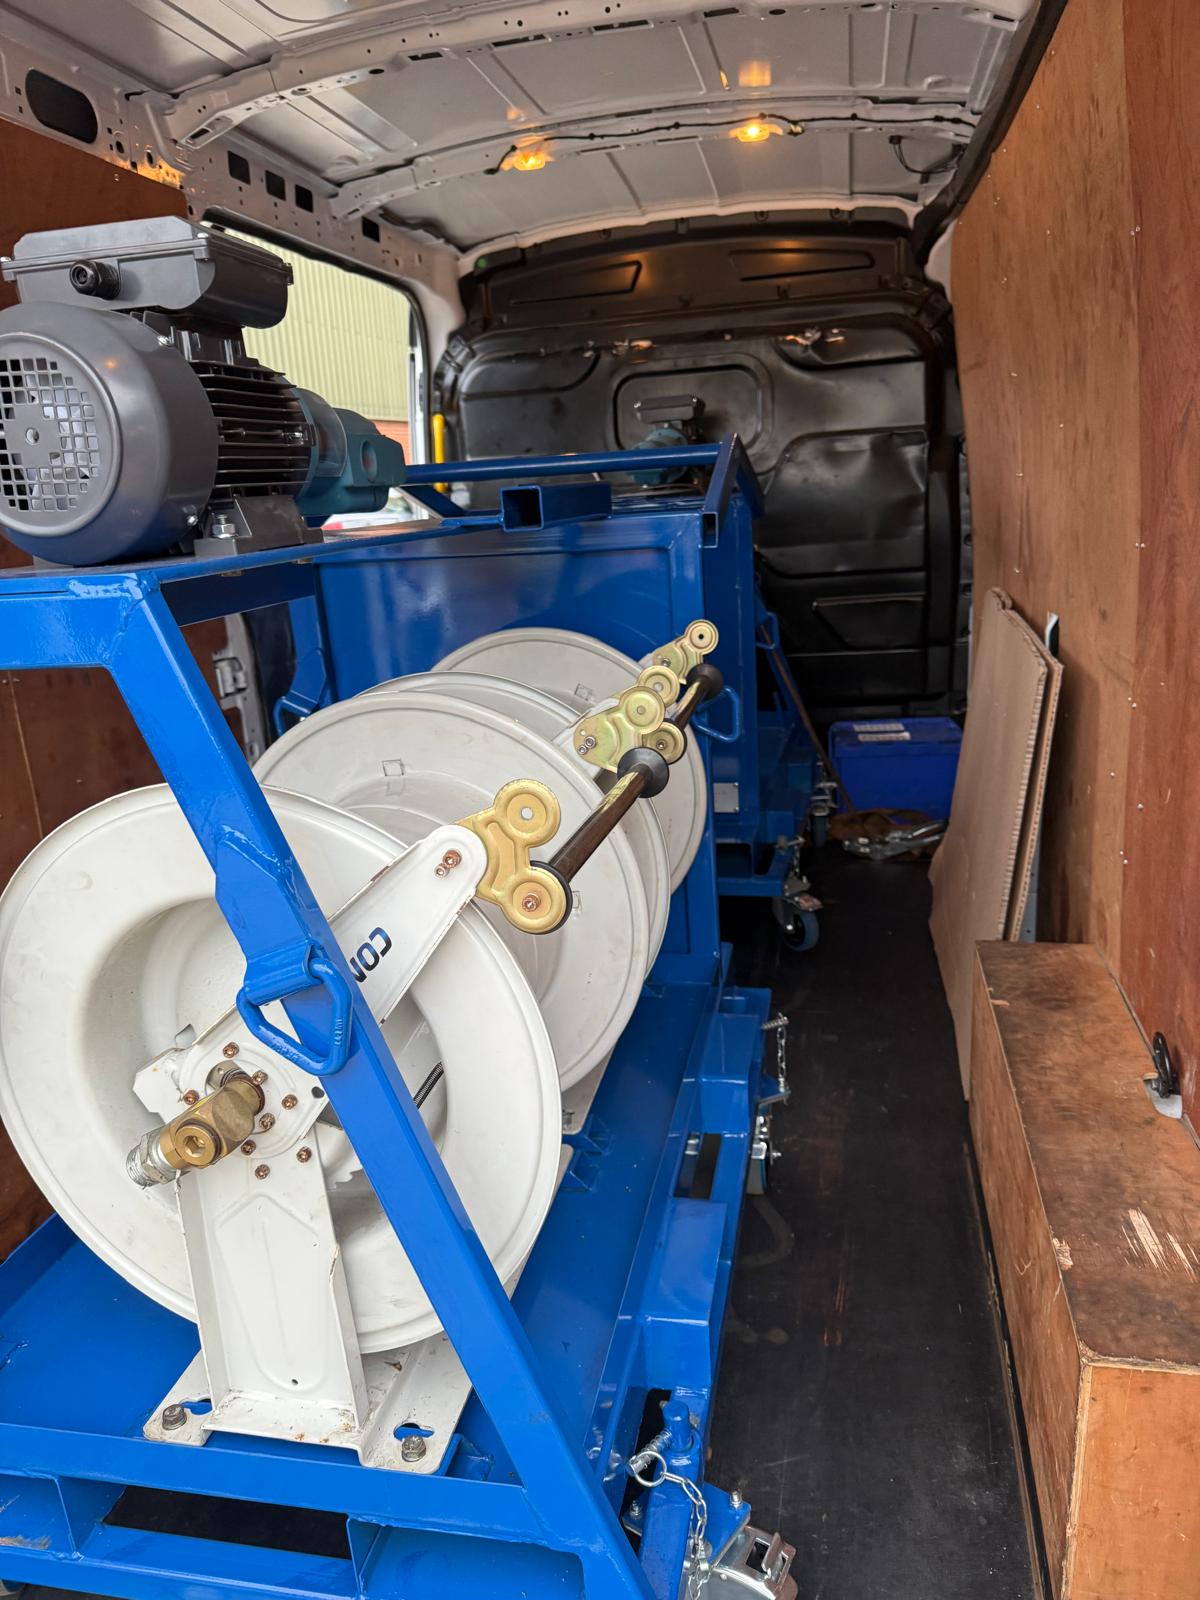
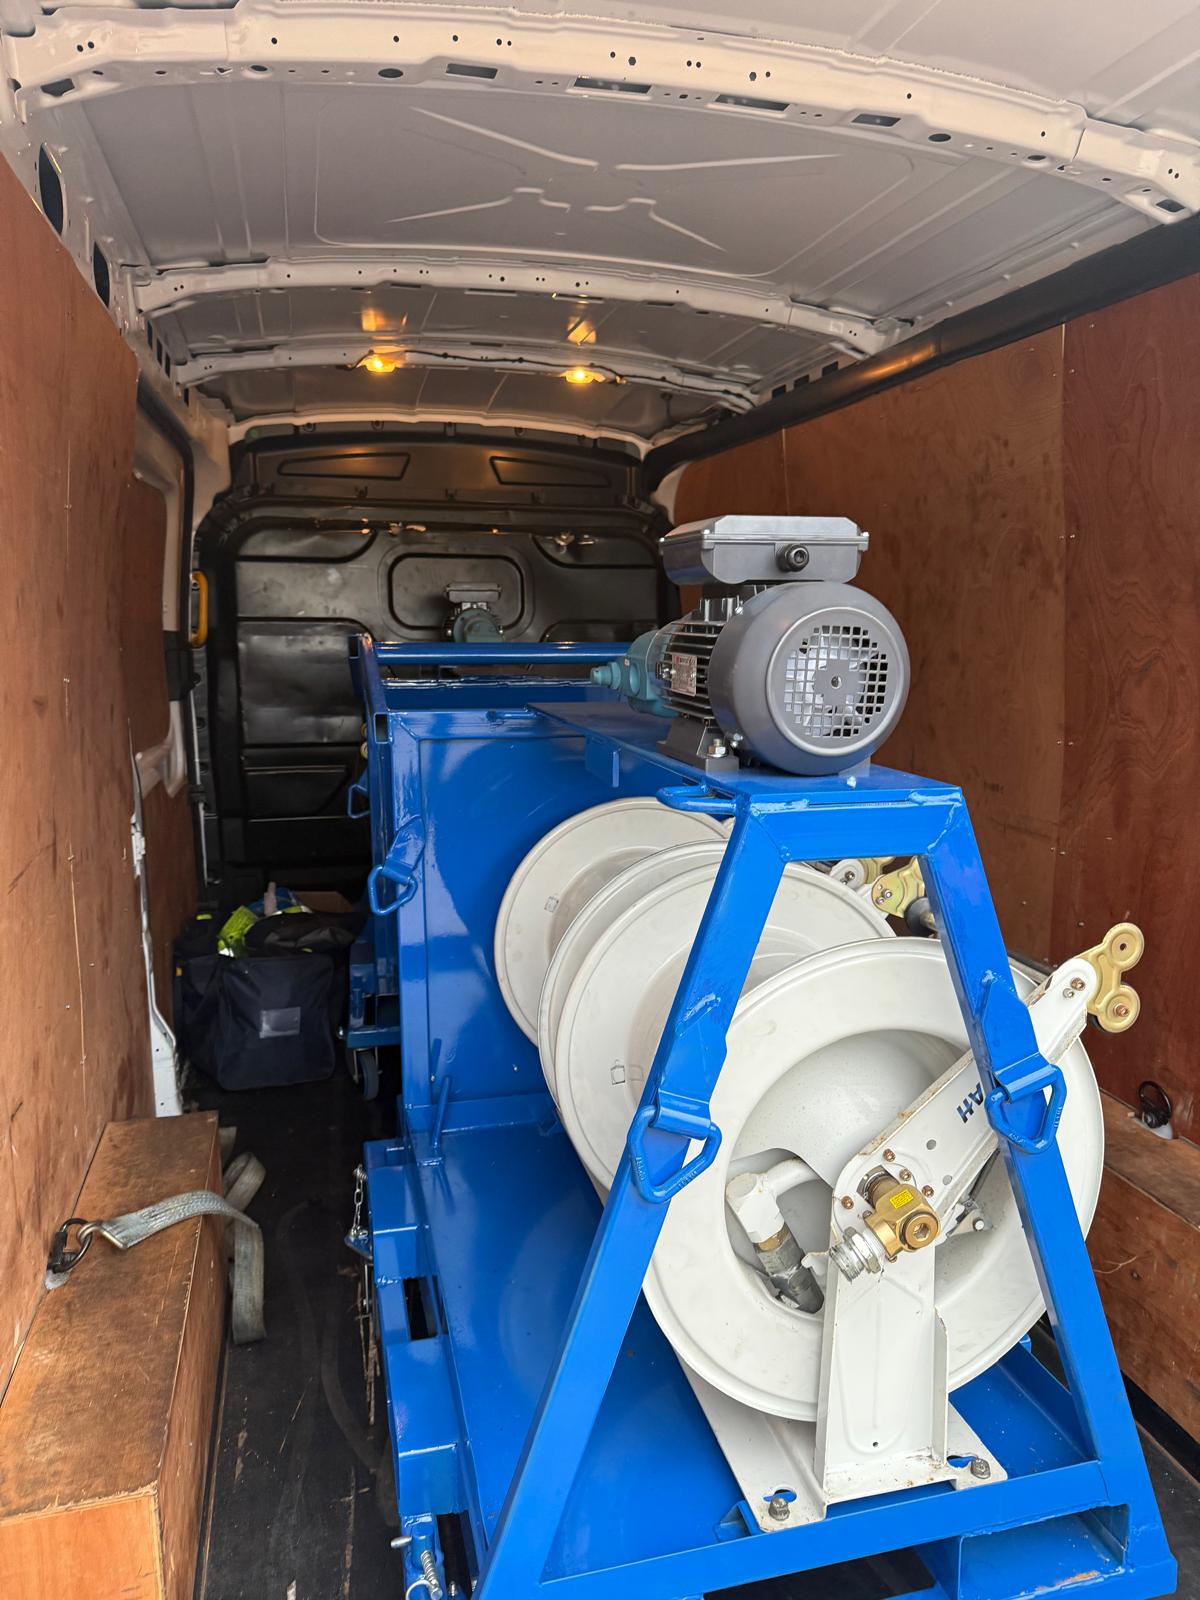
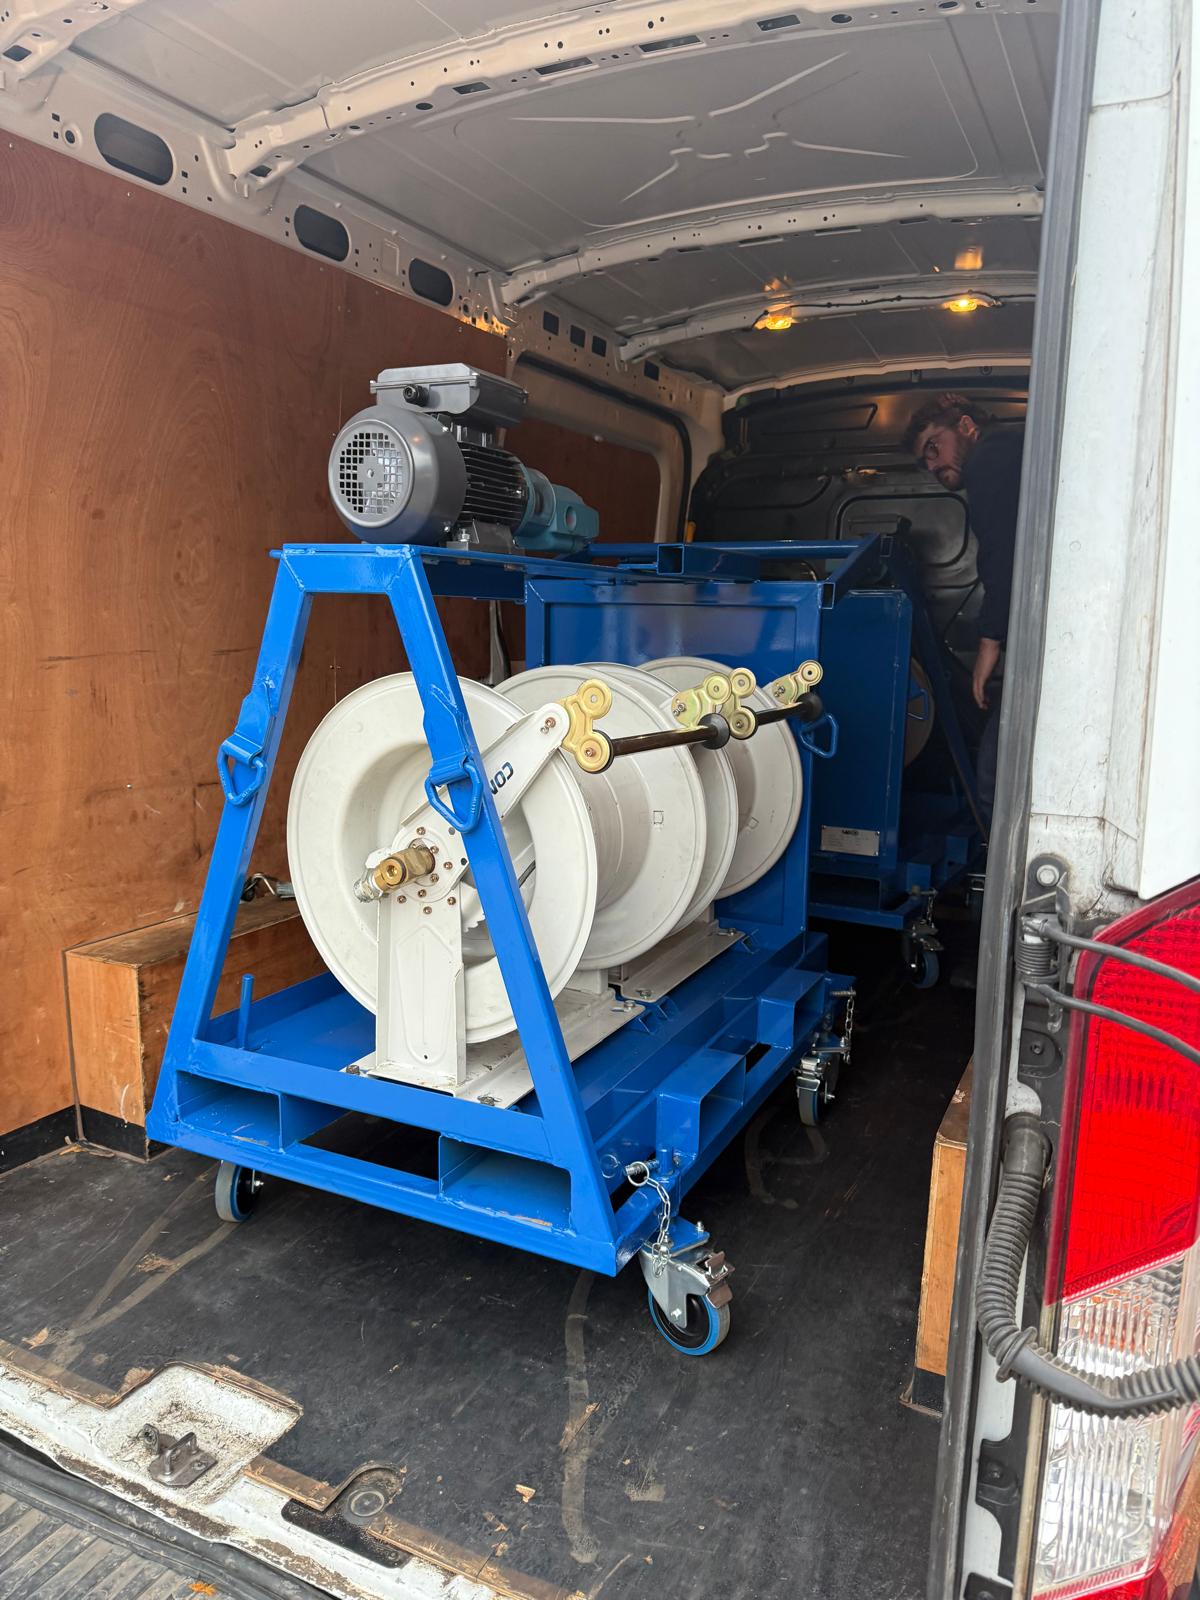
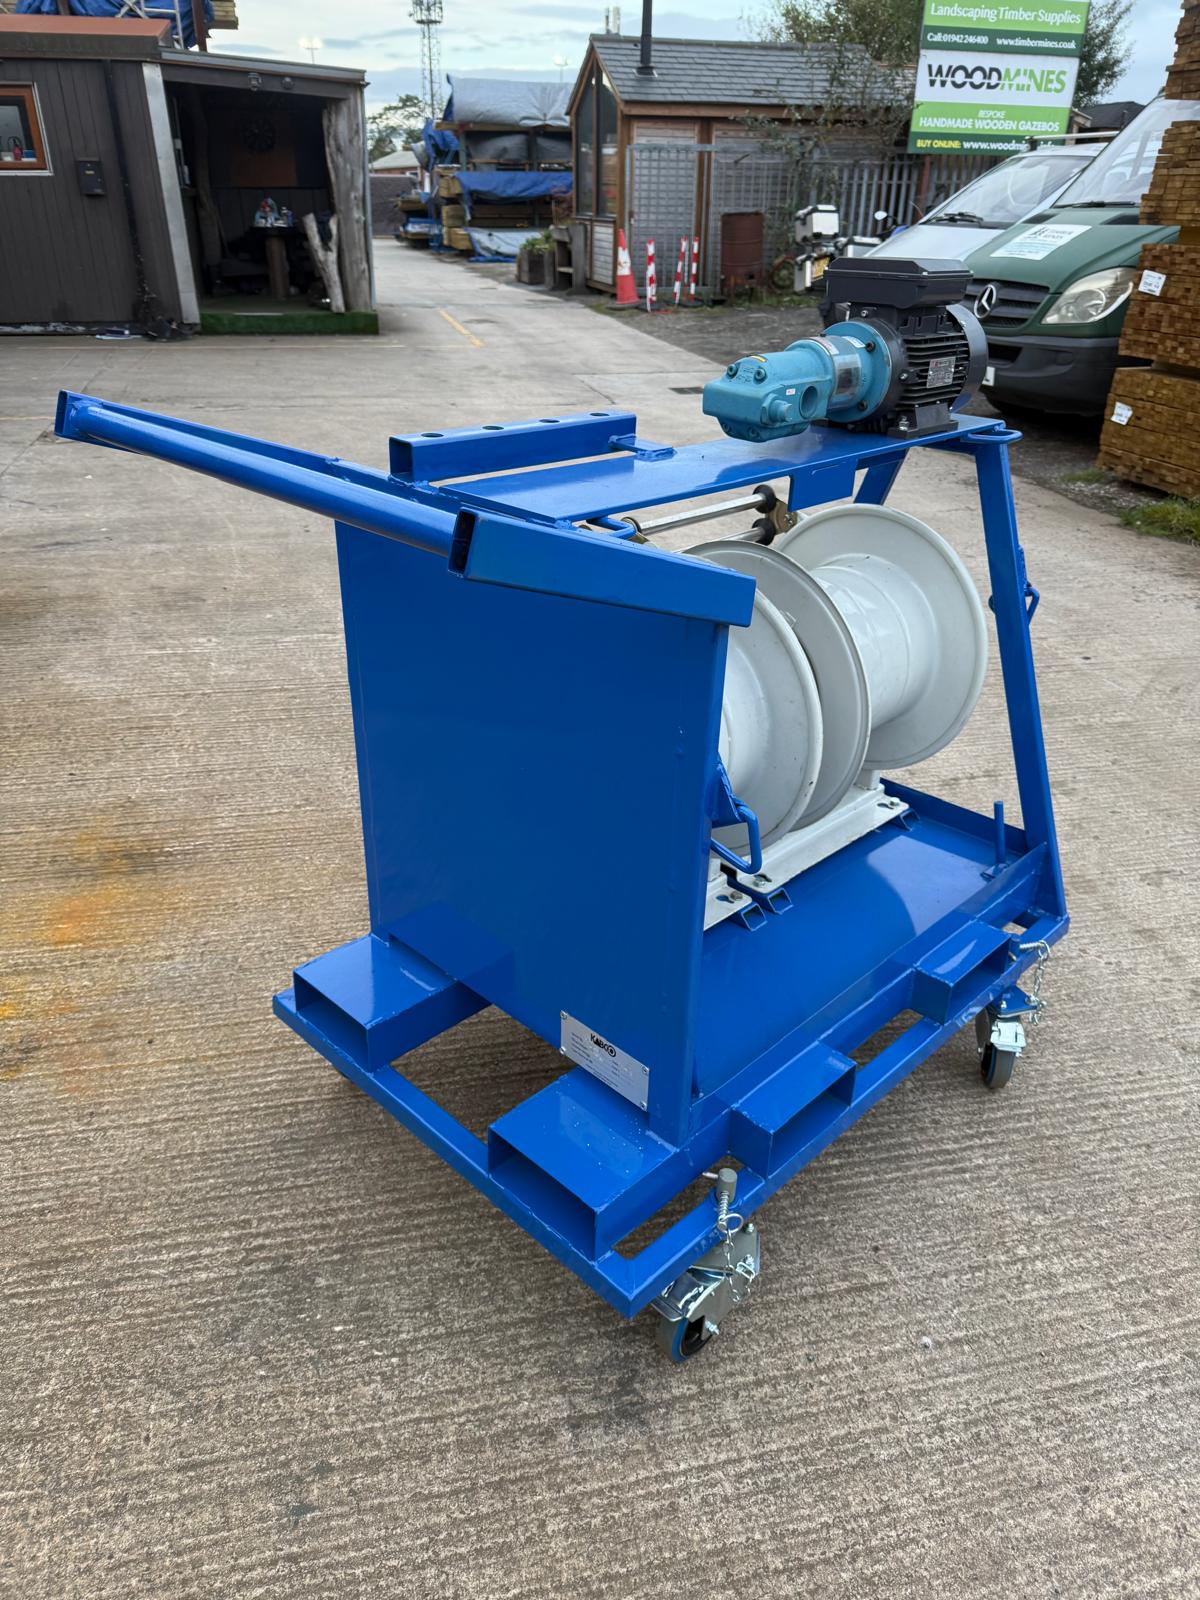
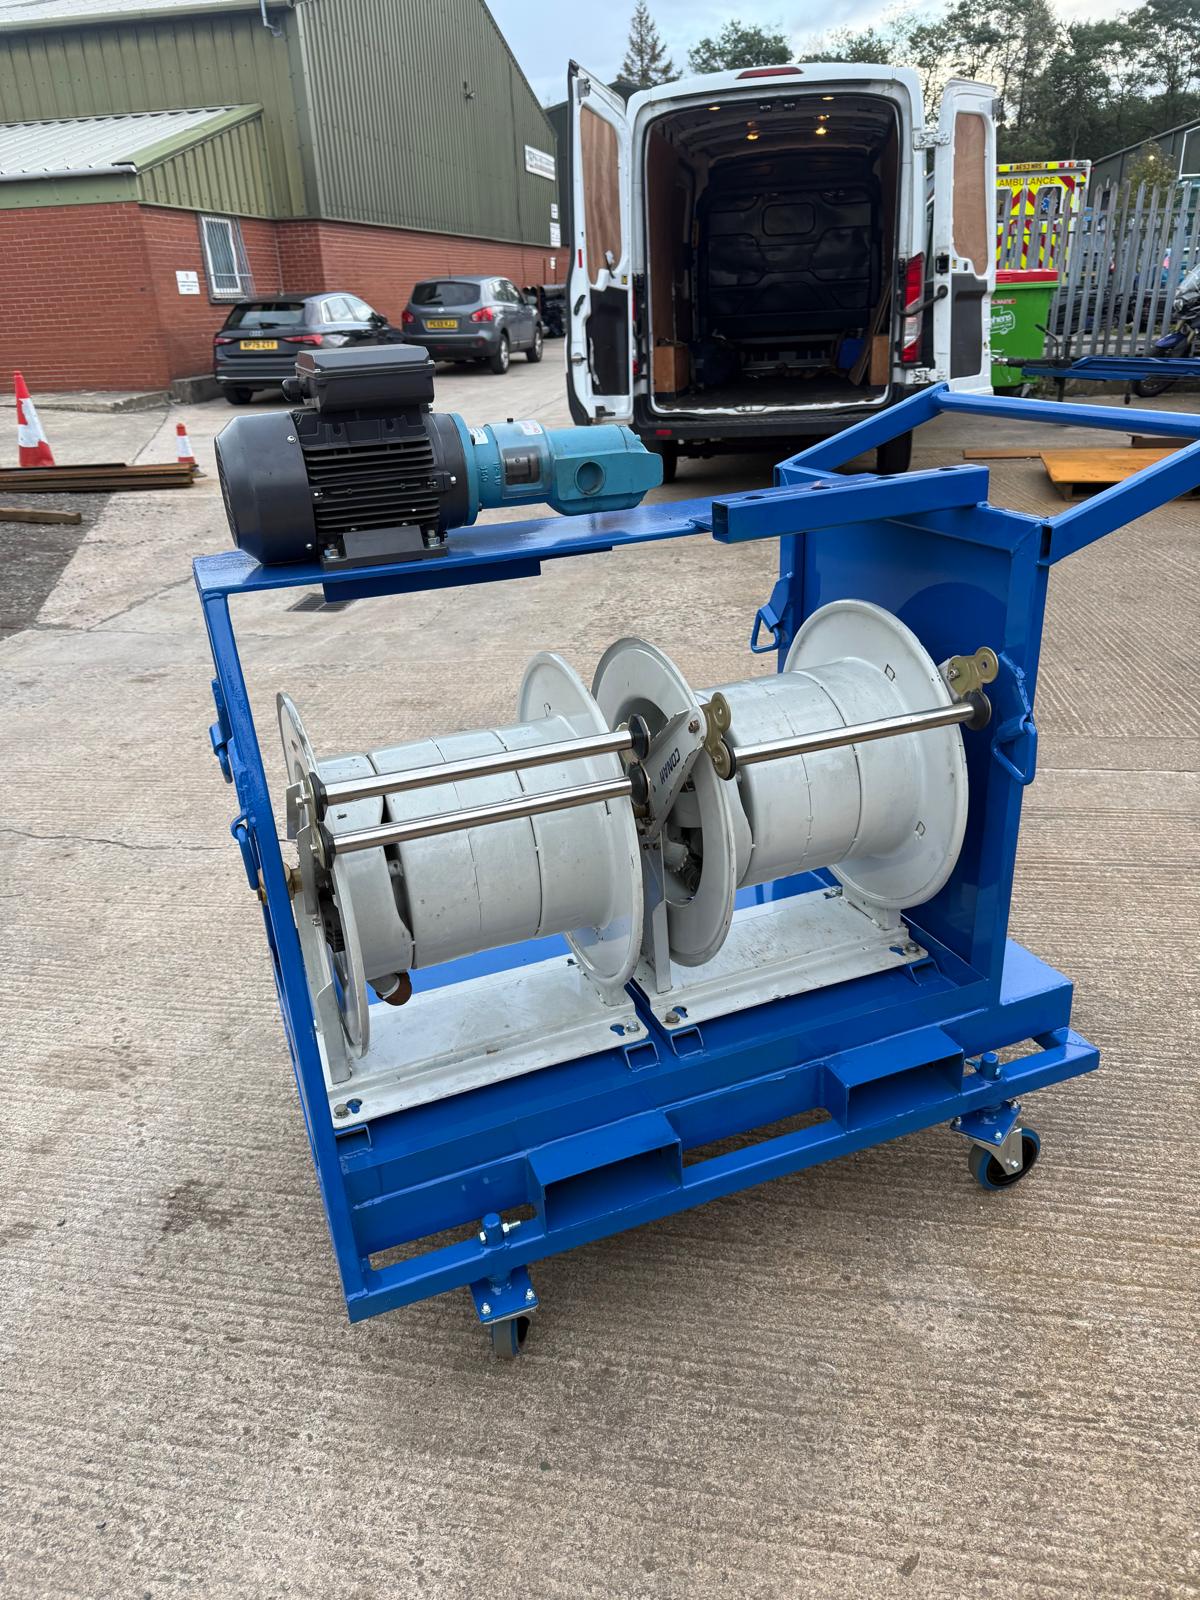
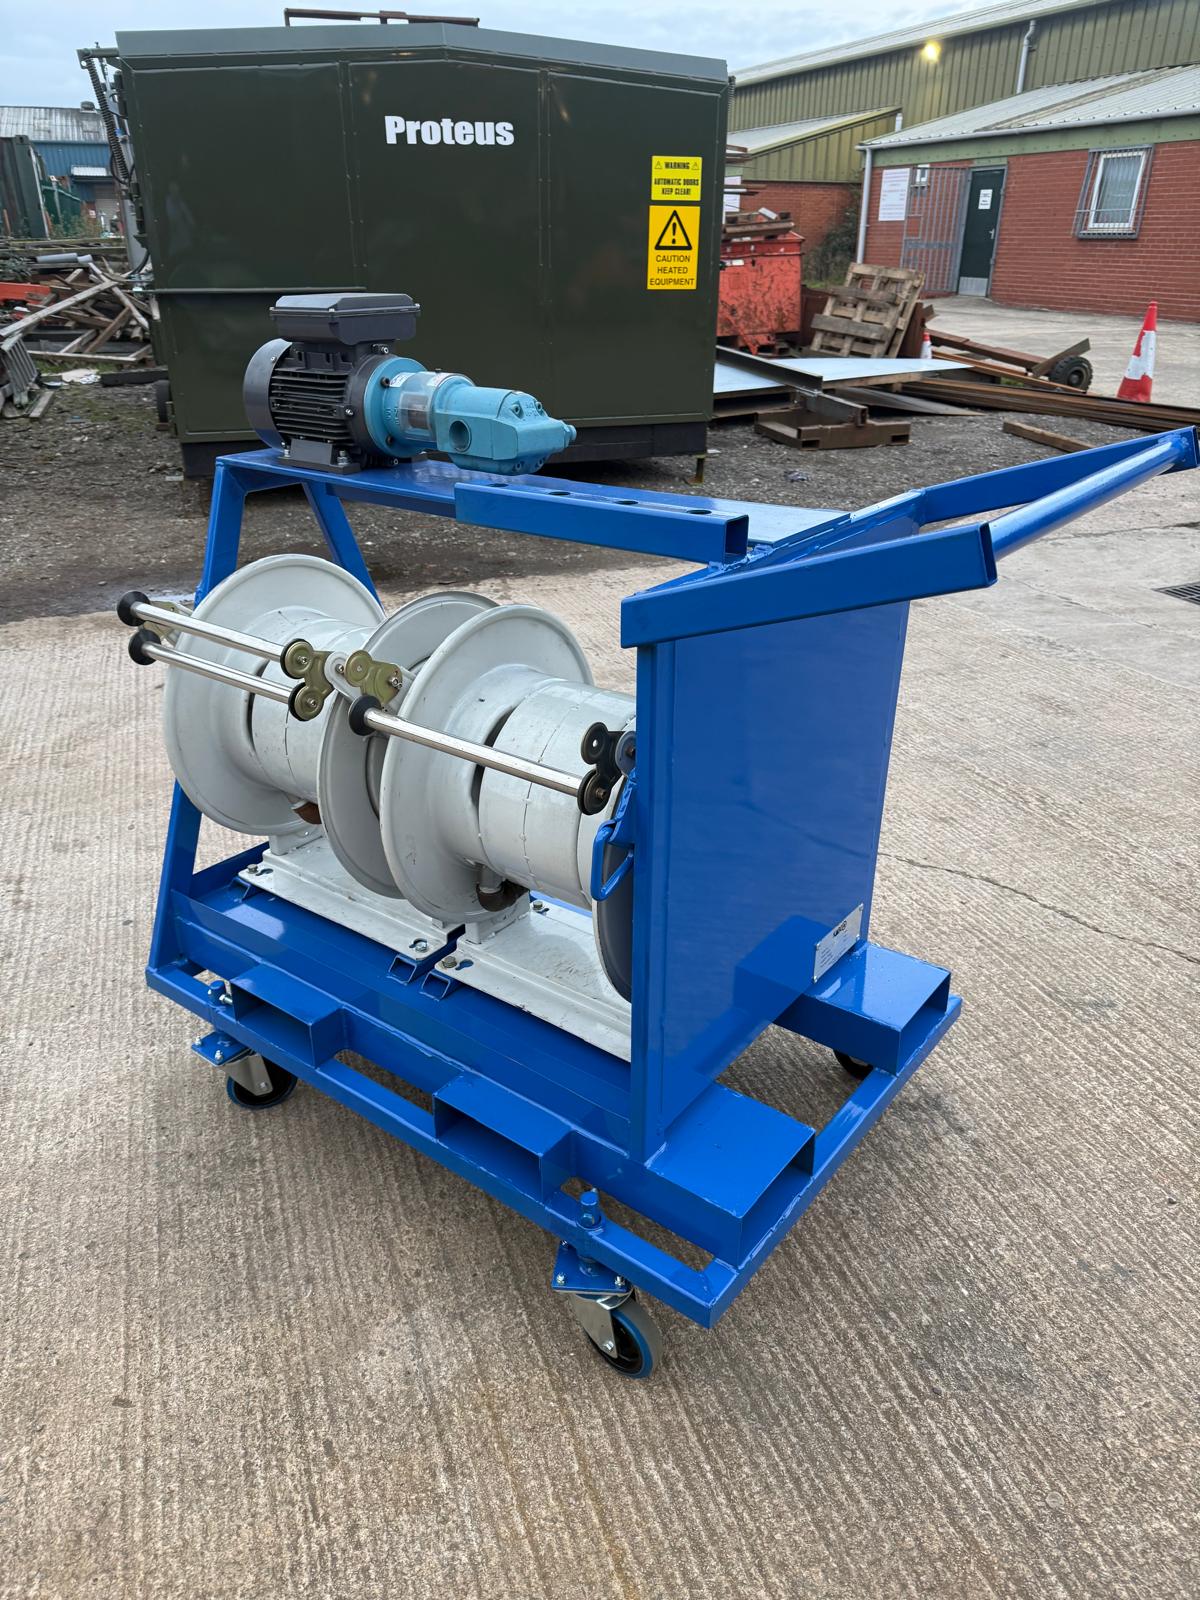
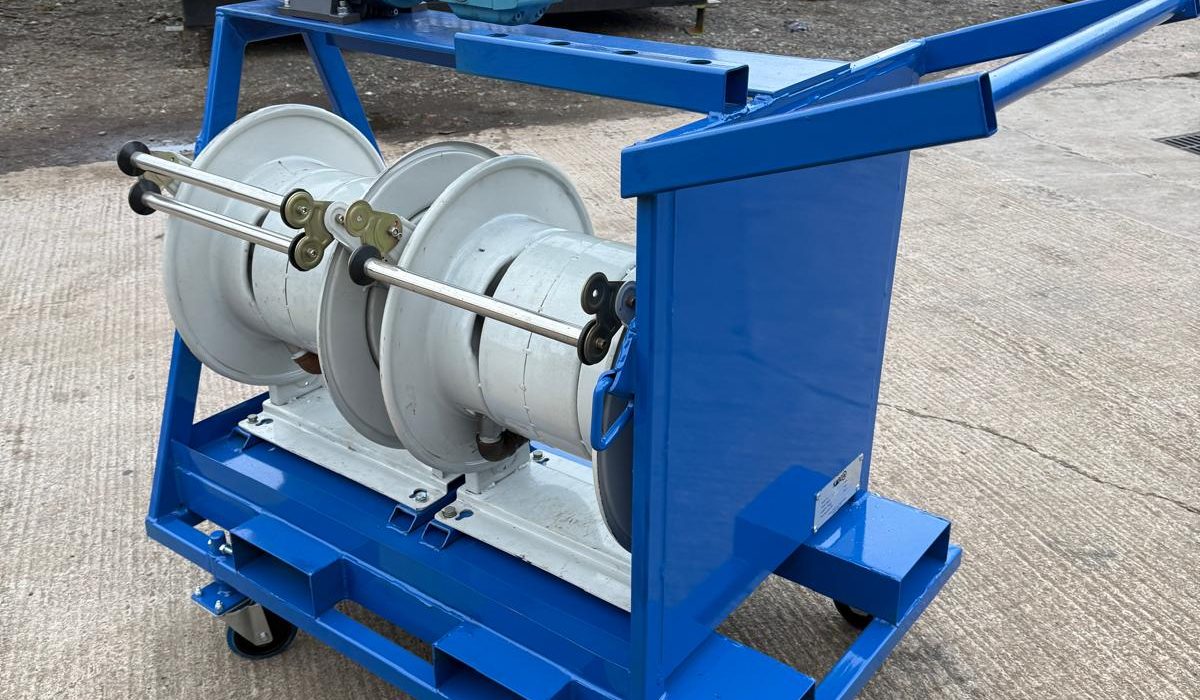
Kabco Fabrications has produced pump trolleys for an oil company, incorporating retractable hose reels, double fork pockets and removable castors.
The trolleys bring together equipment handling and hose storage in a practical fabrication designed around the customer’s operational requirements.
Integrated Retractable Hose Reels
Each trolley incorporates a retractable hose reel, keeping the hose stored on the unit and available for deployment when needed.
Retracting the hose after use helps keep the surrounding work area organised and reduces the amount of loose hose left on the floor. It also makes the trolley easier to move between tasks, with the hose contained within the assembly.
Double Fork Pockets
Double fork pockets provide dedicated points for handling the trolleys with a forklift.
This gives the customer a practical way to move the units over longer distances or between operational areas, alongside the mobility provided by the castors.
Incorporating the pockets into the fabrication makes mechanical handling part of the trolley’s design from the outset.
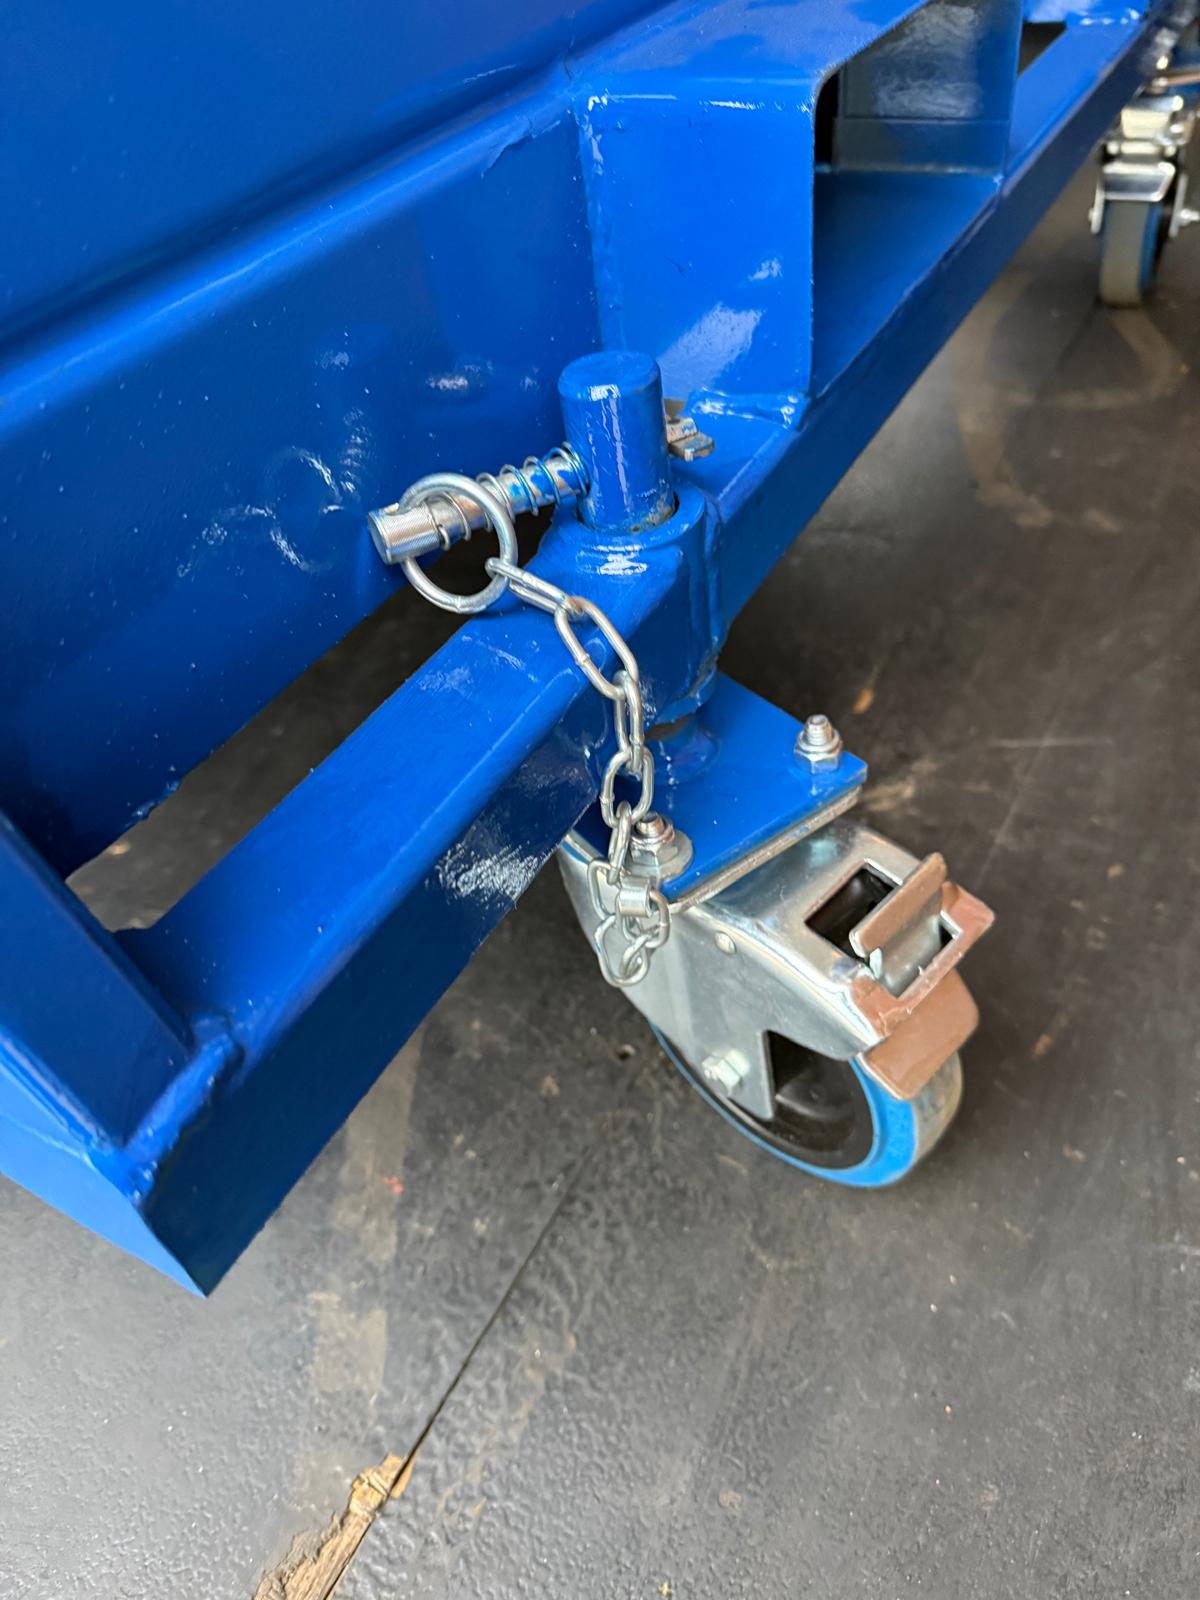
Removable Castors
The removable castors allow the trolleys to be wheeled into position for day-to-day use.
Their removable design also provides flexibility when configuring the units and allows individual castors to be replaced during maintenance without replacing the complete trolley.
Together, the castors and fork pockets provide different handling options to suit the task and location.
Fabrication Around Operational Requirements
Equipment trolleys need to account for how the equipment will be stored, moved, positioned and maintained.
For this project, the combination of retractable hose reels, double fork pockets and removable castors brought those requirements into one assembly. The result is a practical trolley configuration that supports hose management, mobility and access for maintenance.
Kabco Fabrications produced the units around the oil company’s specified requirements, combining the individual features into a purpose-built equipment handling solution.